English


Views: 0 Author: Site Editor Publish Time: 2026-09-14 Origin: Site


A roll can arrive on time and still be unusable if its edges are crushed, its wrap is punctured or its dimensions no longer suit the converting line. Bulky hygiene materials also consume freight space that a weight-only purchasing comparison misses. Effective hygiene material packaging balances cube utilization with product protection, handling limits and the quality checks needed at destination. The unit to optimize is the usable material delivered, not merely the number of rolls loaded.
Record roll diameter, width, core, mass and sensitivity to compression or moisture; design protective wrapping and a stable pallet pattern; then trial the actual route and inspect usable yield on arrival. Avoid assuming that maximum compression minimizes total cost.
Begin with a material-and-roll risk register. Record the surface sensitivity, edge strength, core strength, potential for telescoping, response to compression and any moisture-control requirement established by the supplier specification. Distinguish risks during storage from those during loading: a stack that is stable in a warehouse may shift under acceleration, vibration and repeated handling. Map each risk to a visible arrival check and, when necessary, a functional check on the converting line. For absorbent papers, document whether an exposed edge, torn wrap or condensation triggers quarantine and testing. For elastic materials, check recovery after the planned storage period. This approach avoids treating all bulky rolls as identical freight units simply because their dimensions look similar.
Consider contamination as well as physical damage. A punctured overwrap can admit dust or handling debris even when the roll remains round. Use clean handling areas, suitable protective layers and clear separation between exposed material and pallet surfaces. Inspect packaging before unloading if the container shows water ingress or cargo movement. Photograph the condition before removing wrap so that the evidence is not lost. An appearance defect does not always mean the full roll must be rejected; define whether an outer-layer removal allowance is acceptable and how usable yield will be measured. Conversely, a clean-looking roll can still unwind poorly after compression. Both visual and functional checks belong in the receiving procedure.
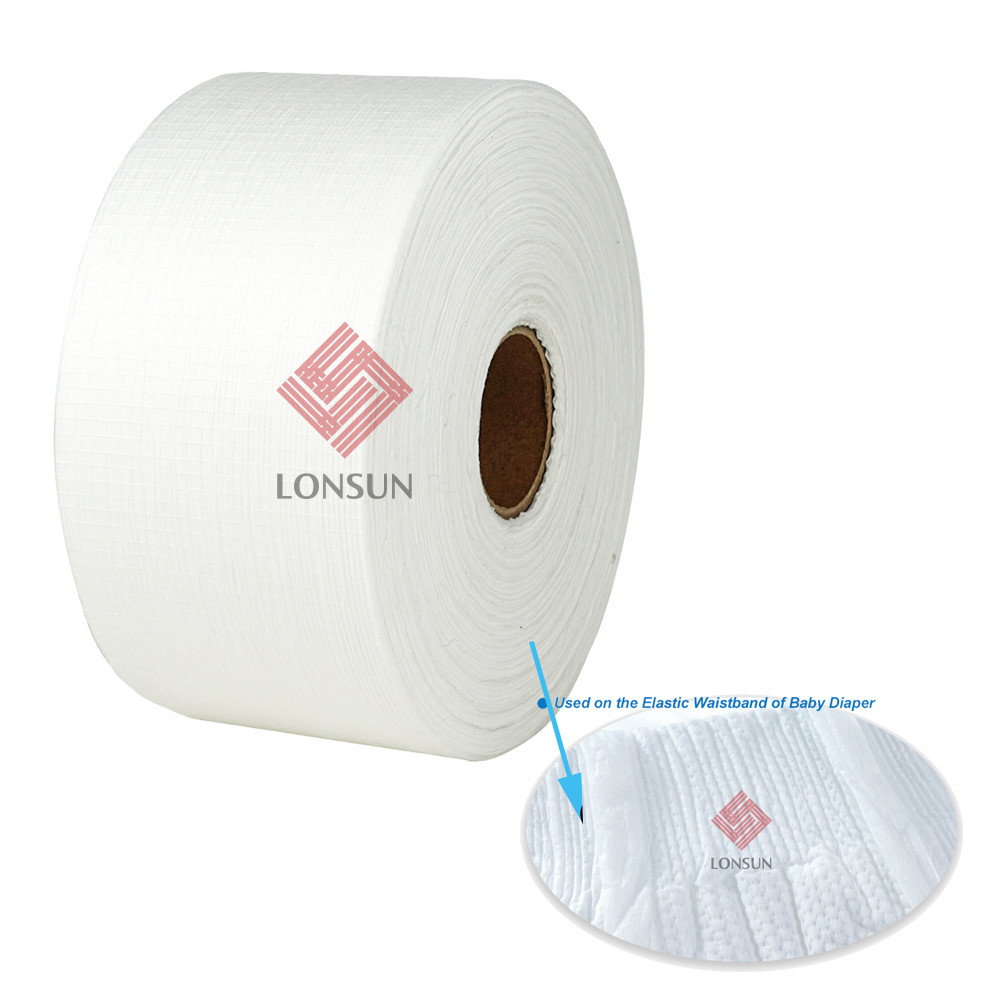
The ultra-thin SAP paper and air-laid absorbent paper are absorbent-component candidates that call for attention to clean, dry storage and protection from damaged wrapping. The elastic diaper nonwoven needs evaluation for compression set and unwind behavior after storage. The crosslap spunlace wipe fabric, a crosslap spunlace substrate, should be checked for edge protection, contamination and dispensing or converting behavior after transport. These are risk questions to test, not blanket claims about any particular shipment.
Document whether a roll may be stacked horizontally or vertically, where lifting force can be applied, and how long a compressed load may remain in storage. The supplier and buyer should agree on core integrity, telescoping, edge deformation and acceptable wrap condition before dispatch.
Specify packaging from the inside outward. Define whether the material needs a sealed inner wrap, end caps or edge guards; then specify roll orientation, spacers, pallet deck and external restraint. Test whether straps create localized deformation and whether stretch wrap actually stabilizes the load without compressing the rolls beyond an agreed limit. A container plan should show the load path and unloading access, not just a theoretical count. Avoid unsupported assumptions about maximum stacking height: it depends on roll mass, pallet construction, warehouse equipment and transit conditions. Put handling symbols and lot labels where they remain visible after palletization. The aim is a pack that can be loaded, counted, protected, received and traced without improvised handling.
Roll geometry affects both transport and conversion. A larger diameter may increase material per roll and reduce line changes, but it can exceed a customer’s lifting or unwind capacity. A narrower roll may fit more efficiently on a pallet but create more splices or trimming at the buyer’s line. Coordinate roll width, core dimensions, maximum mass and allowable splice count with the converter before optimizing pallet layout. Where mixed materials share a shipment, separate them by handling needs and keep labels legible. Review whether a heavy roll can press into a lighter one during a long route. Packaging savings should be evaluated through the entire chain from winding to first use, not at the container door alone.
Check packaging waste and operational safety without making an unsupported environmental claim. More wrap may reduce contamination yet increase unpacking labor and discarded material. A reusable pallet or stronger corner guard may perform well on a closed route but be impractical when return logistics are uncertain. Measure these effects alongside damage and freight, and confirm that any recycling statement matches the actual materials and collection arrangements in the destination market. Train handlers on lifting points and maximum load; a technically sound package can fail when equipment grips a roll through its protective edge. Include photos or diagrams in the shipping specification so warehouse teams do not have to interpret vague wording under time pressure.
Use an inner protective layer appropriate to the material, edge and end protection, and an outer unit that remains stable through lifting and vibration. Label each roll with material code, lot, dimensions, gross and net mass, orientation and handling instructions. A clear scan path from roll to pallet to shipment makes damage investigation and lot segregation easier.
| Packaging choice | Potential gain | Risk to validate |
|---|---|---|
| Larger roll diameter | Fewer changes on the line | Weight, handling and deformation |
| Tighter pallet pattern | Better space use | Edge contact and load stability |
| Added wrap or barrier | Lower contamination exposure | Cost, waste and trapped moisture |
| Compression | More material per shipment | Recovery and usable yield |
Separate fixed shipment costs from variable costs. Container or truck charges, pallet cost and documentation may be largely fixed for a load, while damaged material, labor and disposal depend on the packaging choice. Compare a baseline pack and a candidate pack under the same route and demand assumptions. Calculate fill rate by both volume and mass because a bulky material may reach the container’s space limit well before its weight limit. Then calculate accepted output after inspection and conversion. A higher fill rate is valuable only if the added density does not create more unusable material or unacceptable handling risk. Record assumptions explicitly so a change in freight rate does not silently change the technical conclusion.
A transport trial should include the weakest expected handling steps, such as transfer between carriers, temporary storage or a long final delivery. Use identifiers to record pallet position and roll condition at each inspection point. On arrival, sample rolls from different load positions rather than only the easiest accessible pallet. Measure diameter, edge condition, core deformation and any relevant material property, then run a representative roll at the intended line settings. If a candidate pack fails, determine whether damage came from stacking, moisture, restraint or equipment before adding more packaging everywhere. Targeted protection usually produces a clearer cost decision than an indiscriminate increase in wrap and cardboard.
Build the dispatch specification with the receiving team, not only the shipper. State what evidence must accompany the load, how damaged pallets are isolated, who authorizes partial acceptance and how usable quantity is reconciled. Review performance over several shipments because a single clean arrival cannot establish repeatability across changing weather and handling conditions. Revisit the packaging design when roll geometry, carrier, route or storage time changes. The practical goal is a measurable reduction in delivered cost per accepted unit while maintaining material integrity and line readiness. That is a more durable result than a one-time increase in container fill.
Define a receiving decision tree before the load arrives. An intact wrap and undamaged core may permit routine acceptance; a torn wrap, water mark or displaced roll should trigger segregation and a defined sampling plan. Record the quantity accepted, conditionally accepted and rejected, plus the reason for each disposition. If outer layers are removed, measure that loss in the same unit used for procurement. Send the supplier and carrier prompt, consistent evidence rather than a vague claim that the material was “damaged.” This enables a packaging correction and fair allocation of cost. The record also protects the next order: recurring edge damage can be investigated by pallet position or handling step rather than treated as random variation.
Set a review cadence that joins logistics and production data. Freight invoices alone cannot show whether packaging improved the outcome; pair them with arrival rejects, roll-change time, converting waste and complaints linked to shipment lots. Look for improvements that hold across more than one route or season before adopting a universal pack. Where demand is uncertain, compare the cost of smaller frequent shipments with the storage risk of a large compressed order. Some customers may prefer more frequent replenishment even at a higher nominal freight rate if it preserves material condition and lowers inventory. A packaging specification should therefore include the replenishment pattern and expected storage time, not merely dimensions and wrap type.
When a shipping change is approved, control its revision like a material change. Update packing instructions, pallet drawings, labels, inspection forms and agreed delivery terms together. Mark the first shipments so the receiving team knows which pack is under evaluation. Record any deviation, such as a different pallet supplier or a carrier’s additional transfer, before interpreting the outcome. If the load arrives sound but unwinds poorly, investigate storage duration and compression history rather than declaring the trial successful from appearance alone. The selected solution should have a repeatable specification, an owner and a trigger for requalification. That turns logistics optimization from an isolated freight negotiation into a controlled part of product quality.
Compare pallet footprint, stack height, gross mass, container loading and the receiving location’s equipment limits. A simple decision metric is total delivered cost divided by usable square meters or kilograms accepted after inspection. Include damaged edges, moisture-related rejection, line waste and disposal. The cheapest freight rate can lose its advantage when a high-density pack increases rejection.
Run a shipment trial before standardizing a new pack. Photograph the load before closing, log pallet positions and environmental conditions where relevant, then inspect representative rolls at the destination. Compare arrival condition and line performance with a reference shipment.
Packaging optimization succeeds when more material arrives usable and ready for the line. Specify handling boundaries, test actual routes and revise pallet density only after measuring damage and recovery. Lonsun, a manufacturer and supplier of hygiene raw materials, lists absorbent papers and nonwovens that illustrate why different roll constructions need different shipping checks. A shared dispatch and receiving specification gives both sides a practical basis for improvement.
Define roll and core dimensions, wrap, edge protection, pallet pattern, labeling, handling limits and arrival acceptance criteria.
No; compare freight savings with recovery, damage, rejection and converting waste after storage and transit.
Link roll and pallet IDs to shipment records and record condition at dispatch, arrival and first use.
Only if trials show comparable handling and recovery; material structure and roll geometry can change the result.


